
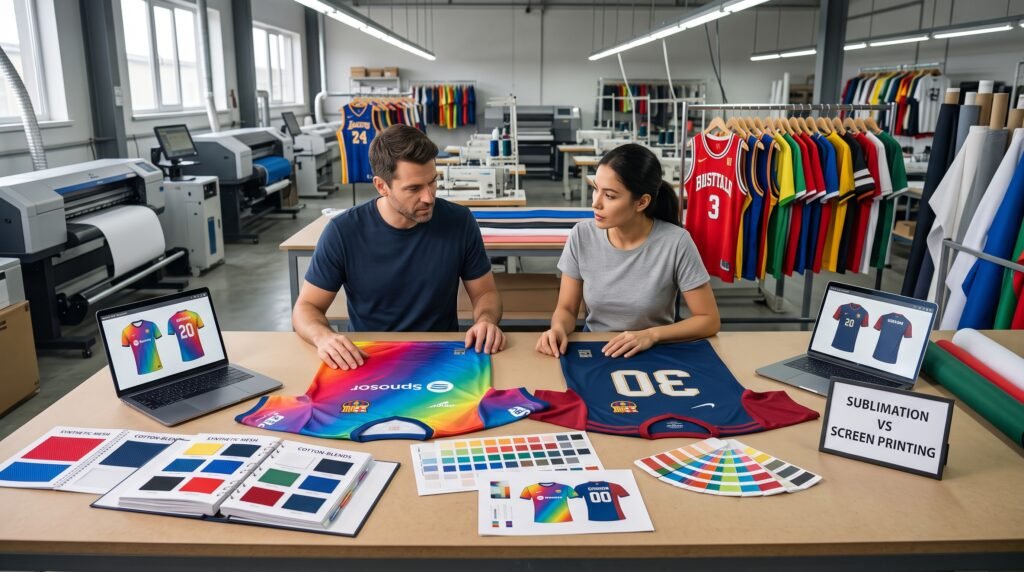
Choosing the right decoration method for your team’s custom uniforms is the difference between jerseys that survive back-to-back seasons and those that peel, crack, or weigh your athletes down.
When outfitting an athletic team, you will inevitably face a choice: Dye Sublimation or Traditional Screen Printing?
Both methods have unique advantages, and the correct choice depends entirely on your team’s budget, sport, aesthetic, and performance requirements. Here is a definitive breakdown to help you make the best choice.
What is Dye Sublimation?
Sublimation is a digital printing technology where your designs, sponsors, and numbers are printed onto transfer paper and then heat-pressed into the fabric at high temperatures.
Instead of sitting on top of the garment, the ink molecularly bonds with the synthetic polyester fibers, essentially dyeing the fabric itself.
The Pros:
-
True Zero-Weight “Hand Feel”: Because the ink becomes one with the fabric, there is absolutely no heavy, rubbery feel. It does not obstruct the breathability, stretch, or lightweight feel of performance mesh.
-
Infinite Visual Complexities: Since the artwork is printed digitally, you can utilize unlimited colors, gradients, custom typography, complex patterns, and sponsor logos for the exact same price.
-
Ultimate Durability: It will never crack, peel, fade, or flake off, even after hundreds of washes and aggressive games.
-
Zero Set-Up Limitations: Ideal for individually personalized roster names and player numbers without additional screen setup fees.
The Cons:
-
Material Constraint: Sublimation only works on polyester (and polyester blends). It will not bond with 100% natural cotton or dark base fabrics unless the polyester itself is dyed.
What is Screen Printing?
Screen printing is a traditional method where thick, vibrant inks (like plastisol or water-based inks) are pressed through a fine mesh stencil (or “screen”) directly onto the surface of the pre-made garment. Each color requires a separate screen, which are applied layer by layer.
The Pros:
-
High Vibrancy & Saturation: Perfect for solid colors, rich metallic finishes, and bold fonts on both natural cotton and synthetic blends.
-
Extremely Cost-Effective at Scale: For bulk orders (typically 50+ units of the exact same design, like simple practice tees), screen printing offers the lowest cost-per-unit.
-
Universal Applications: Screen printing works on virtually any fabric 100% cotton, polyester, poly-blends, fleece, and canvas.
The Cons:
-
The “Sweat Patch” Effect: Heavy inks on the chest can block ventilation, making the jersey heavy, stiff, and uncomfortable during sweat-heavy games.
-
Prone to Wear & Tear: Over time, especially on high-stretching performance fabrics, heavy screen print ink can crack, fade, or peel off when exposed to intense contact, sunlight, and wash cycles.
-
Restrictive Set-Up Costs: Since every color, logo, and name requires a custom stencil, multicolor designs or individual name/number customizations can become extremely expensive.
Feature Comparison: Sublimation vs. Screen Printing
| Feature | Dye Sublimation | Screen Printing |
| Material Fit | Synthetic Polyester Only | Cotton, Polyesters, Fleece, Blends |
| Durability | Permanent (Lifetime of the garment) | Moderate (Prone to cracking/peeling) |
| Design Limits | Unlimited (Gradients, patterns, photo quality) | Best for solid, simple shapes (1-4 colors) |
| Ventilation | 100% Breathable (Zero hand-feel) | Heavy spots can trap heat & block airflow |
| Setup Cost | Low/None | High (Per screen and per color) |
| Bulk Cost-Savings | Flat Pricing | Extremely cheap at high volumes |
| Team Roster Customization | Free & easy (Individual names/numbers) | Expensive (Needs custom screens) |
The Verdict: Which is Best for Your Team?
-
Choose Dye Sublimation if: You are outfitting active, high-intensity teams (soccer, basketball, cycling, lacrosse, rugby) where you need maximum breathability, lightweight movement, complex graphic patterns, and individual player names/numbers that can endure hard wash and wear.
-
Choose Screen Printing if: You are ordering large-scale promotional merchandise, sideline apparel, team hoodies, staff polo shirts, or basic single-color practice jerseys, particularly on cotton or heavy fleece fabrics.